info@hxcnc.com Shenzhen, China Reply within 24 hours
ISO 9001 : 2015 Get Instant Quote
Heterogeneous Material Assembly Specialist · Ships worldwide

Precision CNC Machined
Ceramic & PEEK Mating Metal Seats

Precision CNC machined metal seats for ceramic and PEEK components — CTE-compensated interface clearances, contact surface Ra 0.4 µm, assembly fit ±0.01 mm. Protects brittle ceramic and PEEK parts from assembly-induced stress. For electrostatic chucks, insulating standoffs, and high-purity semiconductor equipment components.

✓ ISO 9001:2015✓ Cleanroom Compatible✓ CMM Verified✓ Helium Leak Test✓ 48h Quote
Precision CNC Machined Ceramic & PEEK Mating Metal Seats
CTE-Compensated
Interface clearance
Ra 0.4µm
Contact surface
±0.01mm
Assembly fit
7 Days
Fastest delivery
CTE Compensated
Interface Clearance temperature range calculated
Ra 0.4µm
Contact Surface protects ceramic/PEEK
±0.01mm
Assembly Fit metal-to-insulator
7 Days
Fastest Delivery
Machining Challenges

Ceramic & PEEK Metal Seat Challenges

The metal seat for a ceramic or PEEK component must protect the brittle material from assembly stress while maintaining precise dimensional relationships across a wide temperature range.

🌡️
CTE Mismatch at the Interface
Aluminium (23 µm/m·K) expands 3.5× more than alumina ceramic (7 µm/m·K) over a 100°C temperature range. The metal seat clearance must be large enough that differential expansion never creates compressive hoop stress on the ceramic — yet tight enough for accurate positioning.
🔩
Assembly Stress Protection
Ceramic and PEEK materials crack under localised point loads. Metal seat design must distribute assembly loads uniformly — no sharp contact edges, no clamping over unsupported spans. HXC designs uniform contact surfaces with specified assembly torque limits.
📐
Precision Positioning
Despite the CTE compensation gap, the ceramic or PEEK component must be positioned accurately. Kinematic seating surfaces — typically three-point contact — provide accurate positioning while allowing CTE expansion in all radial directions.
Our Work

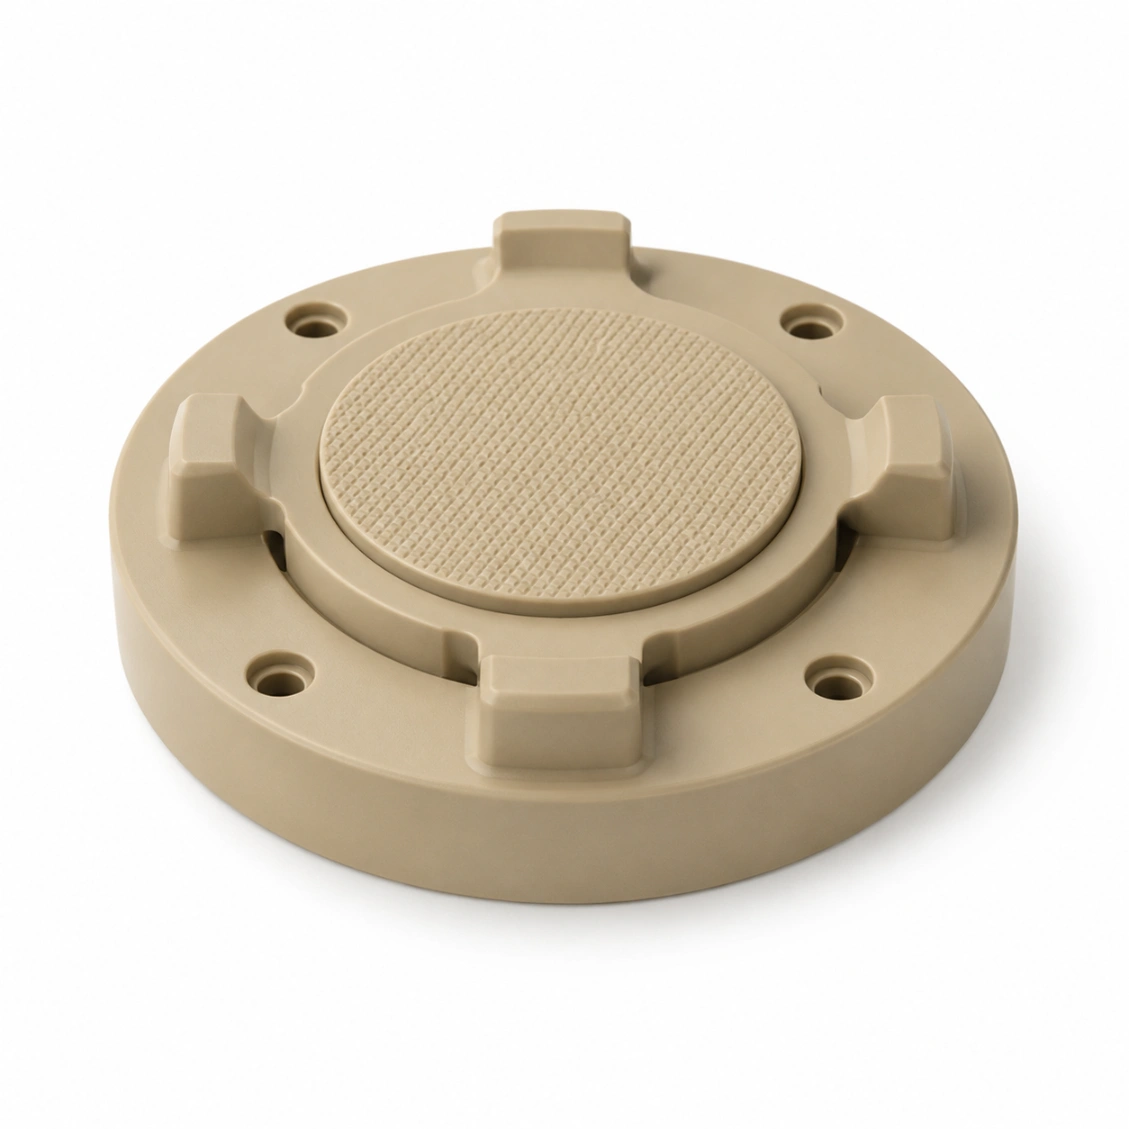
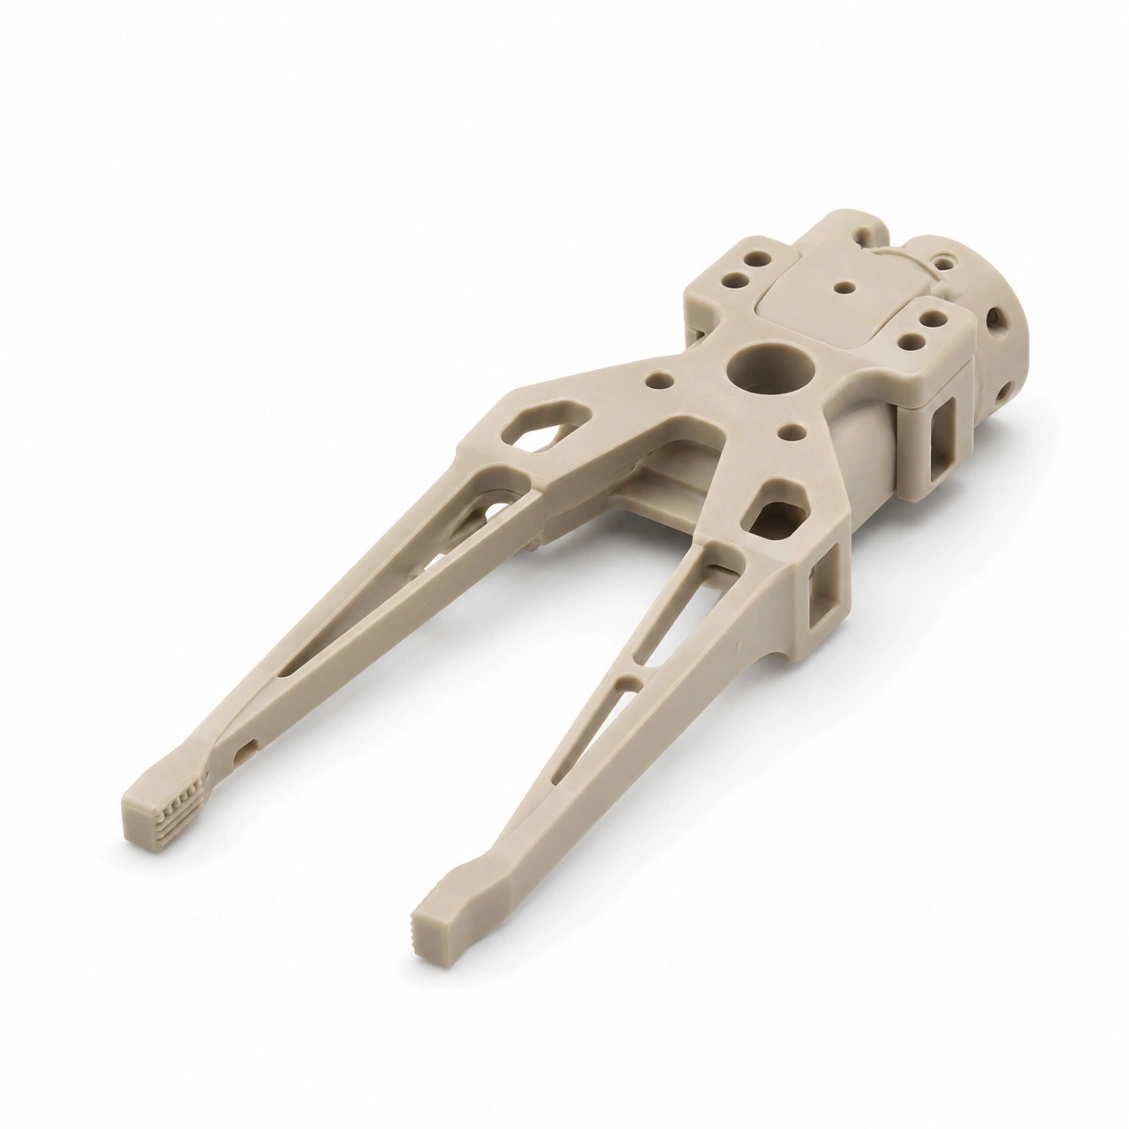
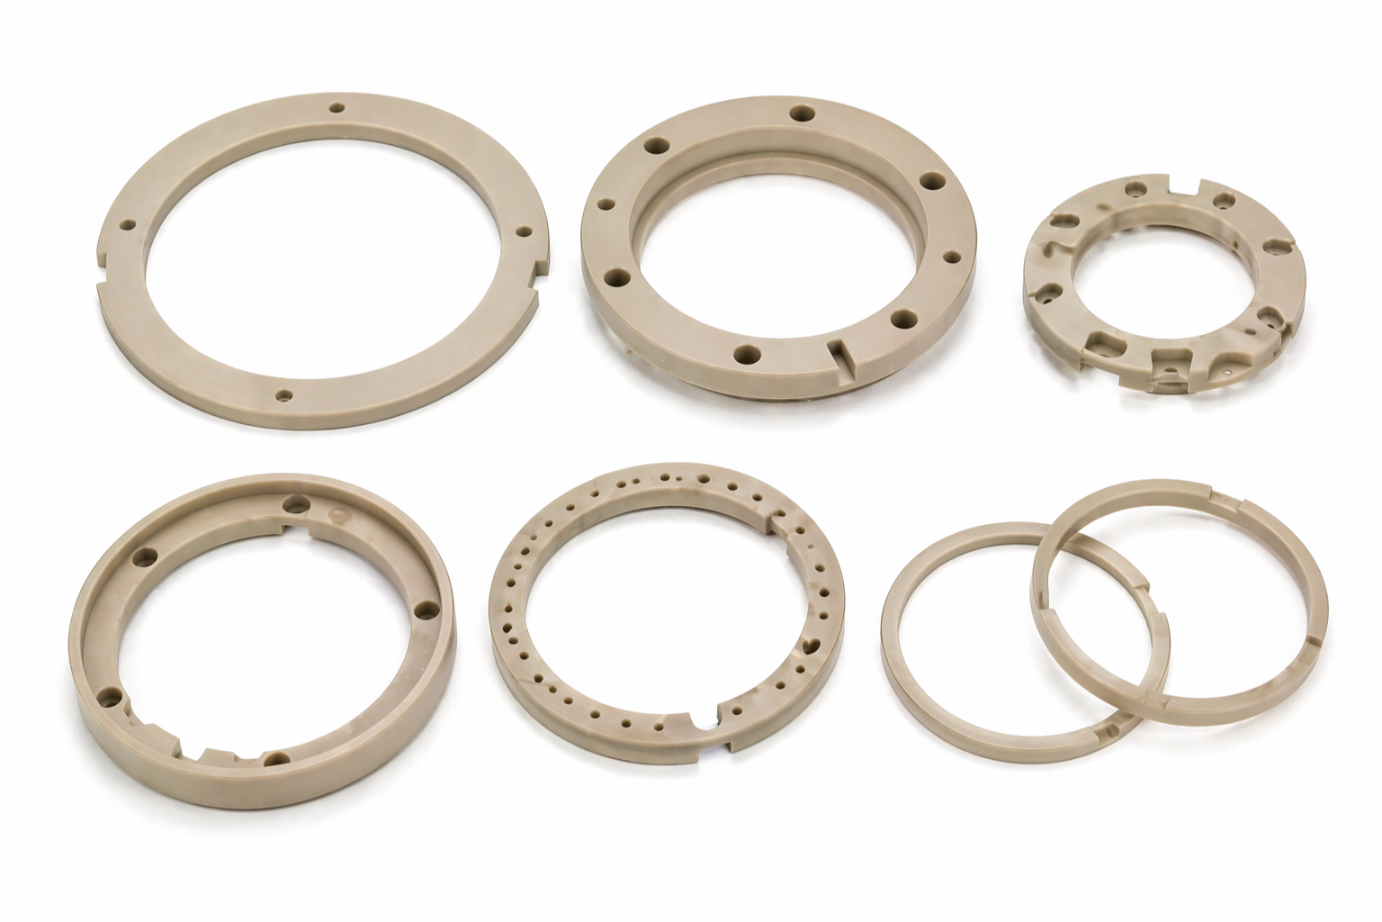
Ceramic & PEEK Mating Metal Seatss We've Made

Real CNC machined semiconductor components — cleaned, inspected, and cleanroom-packaged.
Request Similar Part →
ESC Ceramic Mating Metal Seat
PEEK Component Metal Seat
Insulator Standoff Metal Base
Ceramic Disc Metal Carrier
Lightweight Ceramic Seat
High-Temp Ceramic Seat
Metal Seat + PEEK Kit
Metal Seats — Batch
Capabilities & Tolerances

What We Can Deliver

Typical specifications — confirm exact requirements at enquiry.

CTE compensation Calculated per temperature range and material pair
Assembly fit tolerance ±0.01 mm
Contact surface Ra 0.4 µm
Kinematic contact 3-point or continuous — per design
Temperature range Calculated up to 350°C (material dependent)
Assembly torque Specified with every threaded component
Materials Al 6061/7075, SUS316L, SUS304, Ti Grade 5
CTE analysis Included in DFM for all ceramic/PEEK interfaces
Matched kits Metal seat + ceramic/PEEK assembly available
Lead time (proto) 7–10 days
Lead time (batch) 12–18 days
Assembly instructions Provided with every kit
How It Works

From Drawing to Cleanroom-Ready Part

Upload your drawing — DFM review, machining, cleaning, inspection, and cleanroom packaging within agreed lead time.

01
Upload Drawing
STEP, DXF, PDF. Include material, tolerance, and cleanliness class.
02
DFM & Quote
Free DFM review — sealing face feasibility, thin walls, deburring strategy. Quote in 48 h.
03
Machine, Clean & Inspect
CNC machining, ultrasonic clean, CMM inspection, cleanroom packaging.
04
Ship Worldwide
Full dimensional report + cleaning record enclosed. DHL / FedEx / sea freight.
Reviews

Trusted by Semiconductor Equipment Engineers

★★★★★
"Surface cleanliness and packaging met our cleanroom incoming inspection requirements immediately. Dimensional report matched our CMM check perfectly."
LW
Li Wei
Process Equipment Engineer · Taiwan
★★★★★
"HXC understood the vacuum sealing requirements for our chamber components without lengthy explanation. Lead time was exactly as quoted."
SL
Sophie L.
Equipment Design Engineer · South Korea
★★★★★
"We've sourced wafer handling and chamber parts from HXC for two years. Cleanliness, dimensional accuracy, and batch consistency are excellent."
JT
James T.
Senior Procurement · USA
FAQ

Frequently Asked Questions About Ceramic & PEEK Metal Seat Machining

Engineering and procurement questions answered by our semiconductor components team.

HXC calculates the thermal expansion difference between the metal seat and ceramic/PEEK component over the full operating temperature range (room temperature to maximum process temperature). The seat bore diameter is machined with a clearance large enough that the metal never creates compressive hoop stress on the ceramic at maximum temperature — yet small enough for accurate positioning. Calculation data is included in the DFM report.
Protection measures: (1) Uniform contact surfaces — no sharp edges or step features that create stress concentrations; (2) Specific assembly torque limits engraved or labelled on threaded metal components (ceramic and PEEK crack at torque values that would be normal for all-metal assemblies); (3) Assembly instructions provided — including recommended torque sequence, assembly tool type, and temperature-dependent re-torque schedule.
HXC recommends three-point kinematic contact (three raised pads on the seat face, each Ra 0.4 µm, at equal 120° spacing) for ceramic disc components. This provides accurate, repeatable positioning while allowing the ceramic to expand or contract radially without constraint. For rectangular ceramic components: four-corner support pads with the same kinematic principle.
Yes — HXC supplies complete matched kits : metal seat + ceramic or PEEK component (sourced from HXC's supply chain or customer-furnished) + assembly hardware + assembly instructions. All components are dimensionally verified as a matched set. Assembly compatibility (clearances at room temperature and at maximum operating temperature) is confirmed before shipment.
SUS316L (to 300°C) : standard for most semiconductor process temperatures. Inconel 625 (to 500°C+) : for high-temperature process applications where Al and standard stainless cannot be used. Al 6061 : for room-temperature and mild-process-temperature applications where weight is important. Material selection depends on process temperature, process chemistry, and the specific ceramic or PEEK material used.
After assembly, HXC performs: (1) Visual inspection — no cracking, no visible stress whitening in PEEK, no chipping; (2) CMM measurement of the assembled component position relative to the seat datum; (3) Cold-cycle test (for temperature-critical applications) — assemble, cool to minimum operating temperature, warm to maximum operating temperature, verify position and inspect for damage.
Prototype: 7–10 days. Matched kits: 8–12 days. Batch: 12–18 days.
Get a Quote

Send Your Drawing.
Get a Quote.

Every enquiry includes a DFM review — tolerance feasibility, material confirmation, and process approach confirmed before production starts. MOQ 1 piece.

24hr
Quote Response
MOQ 1
Prototypes OK
ISO
9001:2015
📐
DFM Review on Every Enquiry
Tolerance feasibility, fixturing strategy, and material confirmation. Specific, actionable feedback — not generic pushback.
🎯
First Article Inspection — Standard
FAI report on every new run. Material certs and surface treatment certs included with every shipment.
🔄
Same Process: Prototype to Production
Process plan from your prototype applies to production batches. No re-qualification when you scale.
⚙
3 / 4 / 5-Axis CNC + Turning
Complex structural parts, shafts, housings, and transmission components. Metals and engineering plastics.
ISO 9001:2015 3/4/5-Axis Milling CNC Turning CMM Inspection Global Delivery