info@hxcnc.com Shenzhen, China Reply within 24 hours
ISO 9001 : 2015 Get Instant Quote
Home/ Products/ Alloy Steel Power Transmission Parts
Product Category
Heat Treatment Managed
ALS / 001 — 025

Alloy Steel
Power Transmission
Parts

25 product lines in 42CrMo, 40Cr, 20CrMnTi, and GCr15 — transmission shafts, spline shafts, gear shafts, connecting rods, couplings, carburised gears, and high-load joints. Every part heat-treated. Every certificate delivered.

25
Product Lines
1080MPa
42CrMo Q&T
HRC 58–62
Case Carburised
PART DWG · ALS-000 COMPOSITION ISO 9001 : 2015
42CrMo Q&T HRC 32
Case HRC 58–62
DIN 5480 Class 7
SPLINE DIN 5480 · TIR ≤0.01 CARBURISED GEAR CON ROD · CL ±0.02 GCr15 BUSHING · HRC 60
42CrMo · 20CrMnTi · GCr15
Main Grades
Q&T · Carburise · Nitride
Heat Treatment
24hr Quote · MOQ 1
Response
25
Product Lines
1080MPa
42CrMo Q&T
HRC 58–62
Case Carburised
H/T Managed
End-to-End
24hr
Quote Turnaround
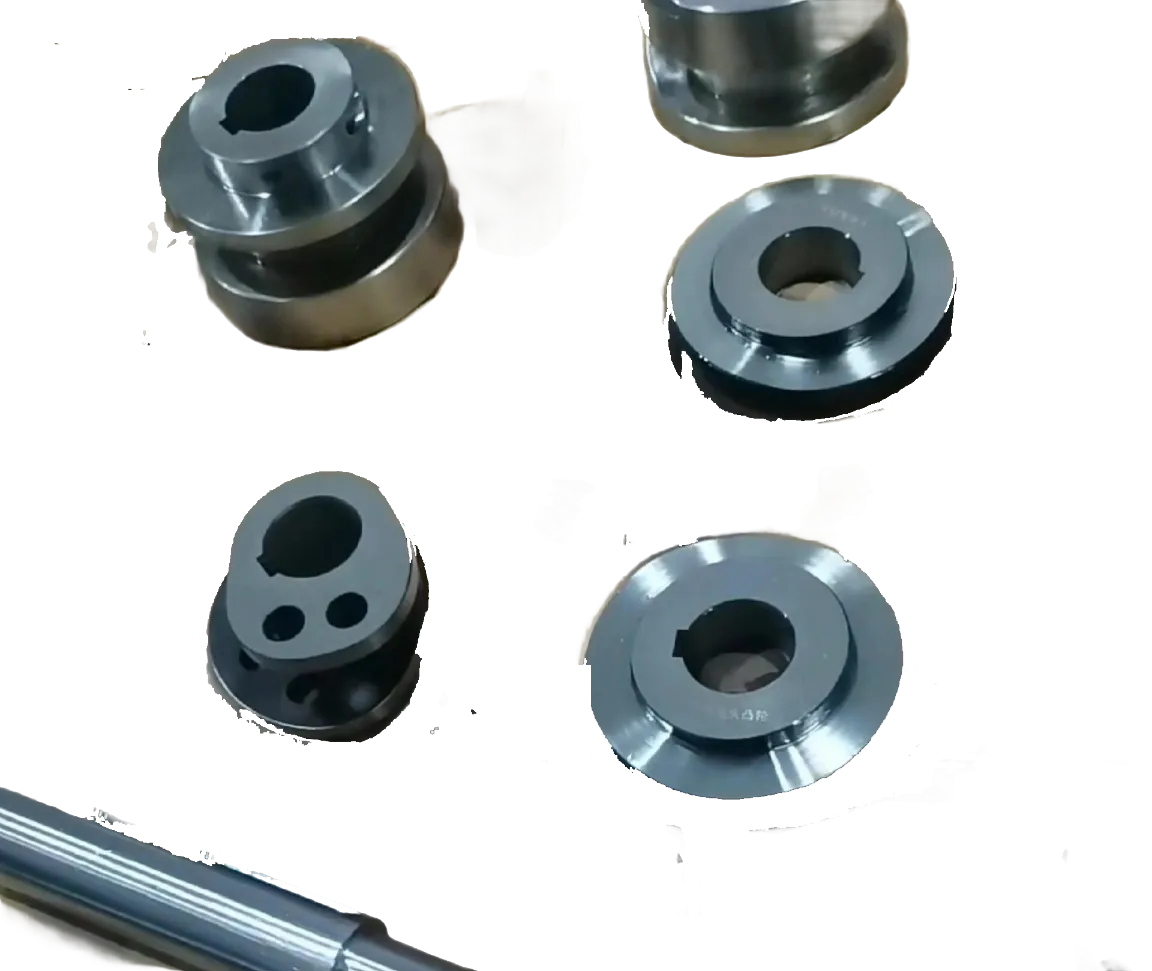
High-Strength Transmission Shaft ✦ Input Shaft ✦ Output Shaft ✦ Spline Shaft ✦ Gear Shaft ✦ Connecting Rod ✦ Fork Connector ✦ Steering Connector ✦ High-Strength Coupling ✦ Flanged Sleeve ✦ Gear Blank ✦ Sprocket ✦ Cam ✦ Eccentric Wheel ✦ Drive Sleeve ✦ Wear-Resistant Bushing ✦ Carburised Gear ✦ Robot Arm Load Joint ✦ Hydraulic Connector ✦ Automotive Component ✦ High-Strength Transmission Shaft ✦ Input Shaft ✦ Output Shaft ✦ Spline Shaft ✦ Gear Shaft ✦ Connecting Rod ✦ Fork Connector ✦ Steering Connector ✦ High-Strength Coupling ✦ Flanged Sleeve ✦ Gear Blank ✦ Sprocket ✦ Cam ✦ Eccentric Wheel ✦ Drive Sleeve ✦ Wear-Resistant Bushing ✦ Carburised Gear ✦ Robot Arm Load Joint ✦ Hydraulic Connector ✦ Automotive Component ✦
Full Product Range

25 Alloy Steel
Transmission & Structural Parts

Select a category tab · 42CrMo · 40Cr · 20CrMnTi · Heat treatment managed · MOQ 1 piece
Request All Products →
Product Categories
Alloy Steel Transmission Shafts Input Output Spline Gear CNC
Transmission Shafts5 Products · ALS-001 to 005Quote →
Five alloy steel transmission shaft product lines for power drive trains — high-strength, input, output, spline, and gear shafts. Bearing seat OD tolerance k6/m6; TIR ≤0.01 mm between seats. Spline shafts hobbed to DIN 5480 class 7. Gear shafts with pinion integral; teeth hobbed and case carburised to HRC 58–62. 42CrMo Q&T to 950–1080 MPa standard.
42CrMo Transmission Shaft CNC Alloy Steel Q&T Bearing Seat Keyway
ALS-001
SHAFTS / 001 — FEATURED
High-Strength Transmission Shafts
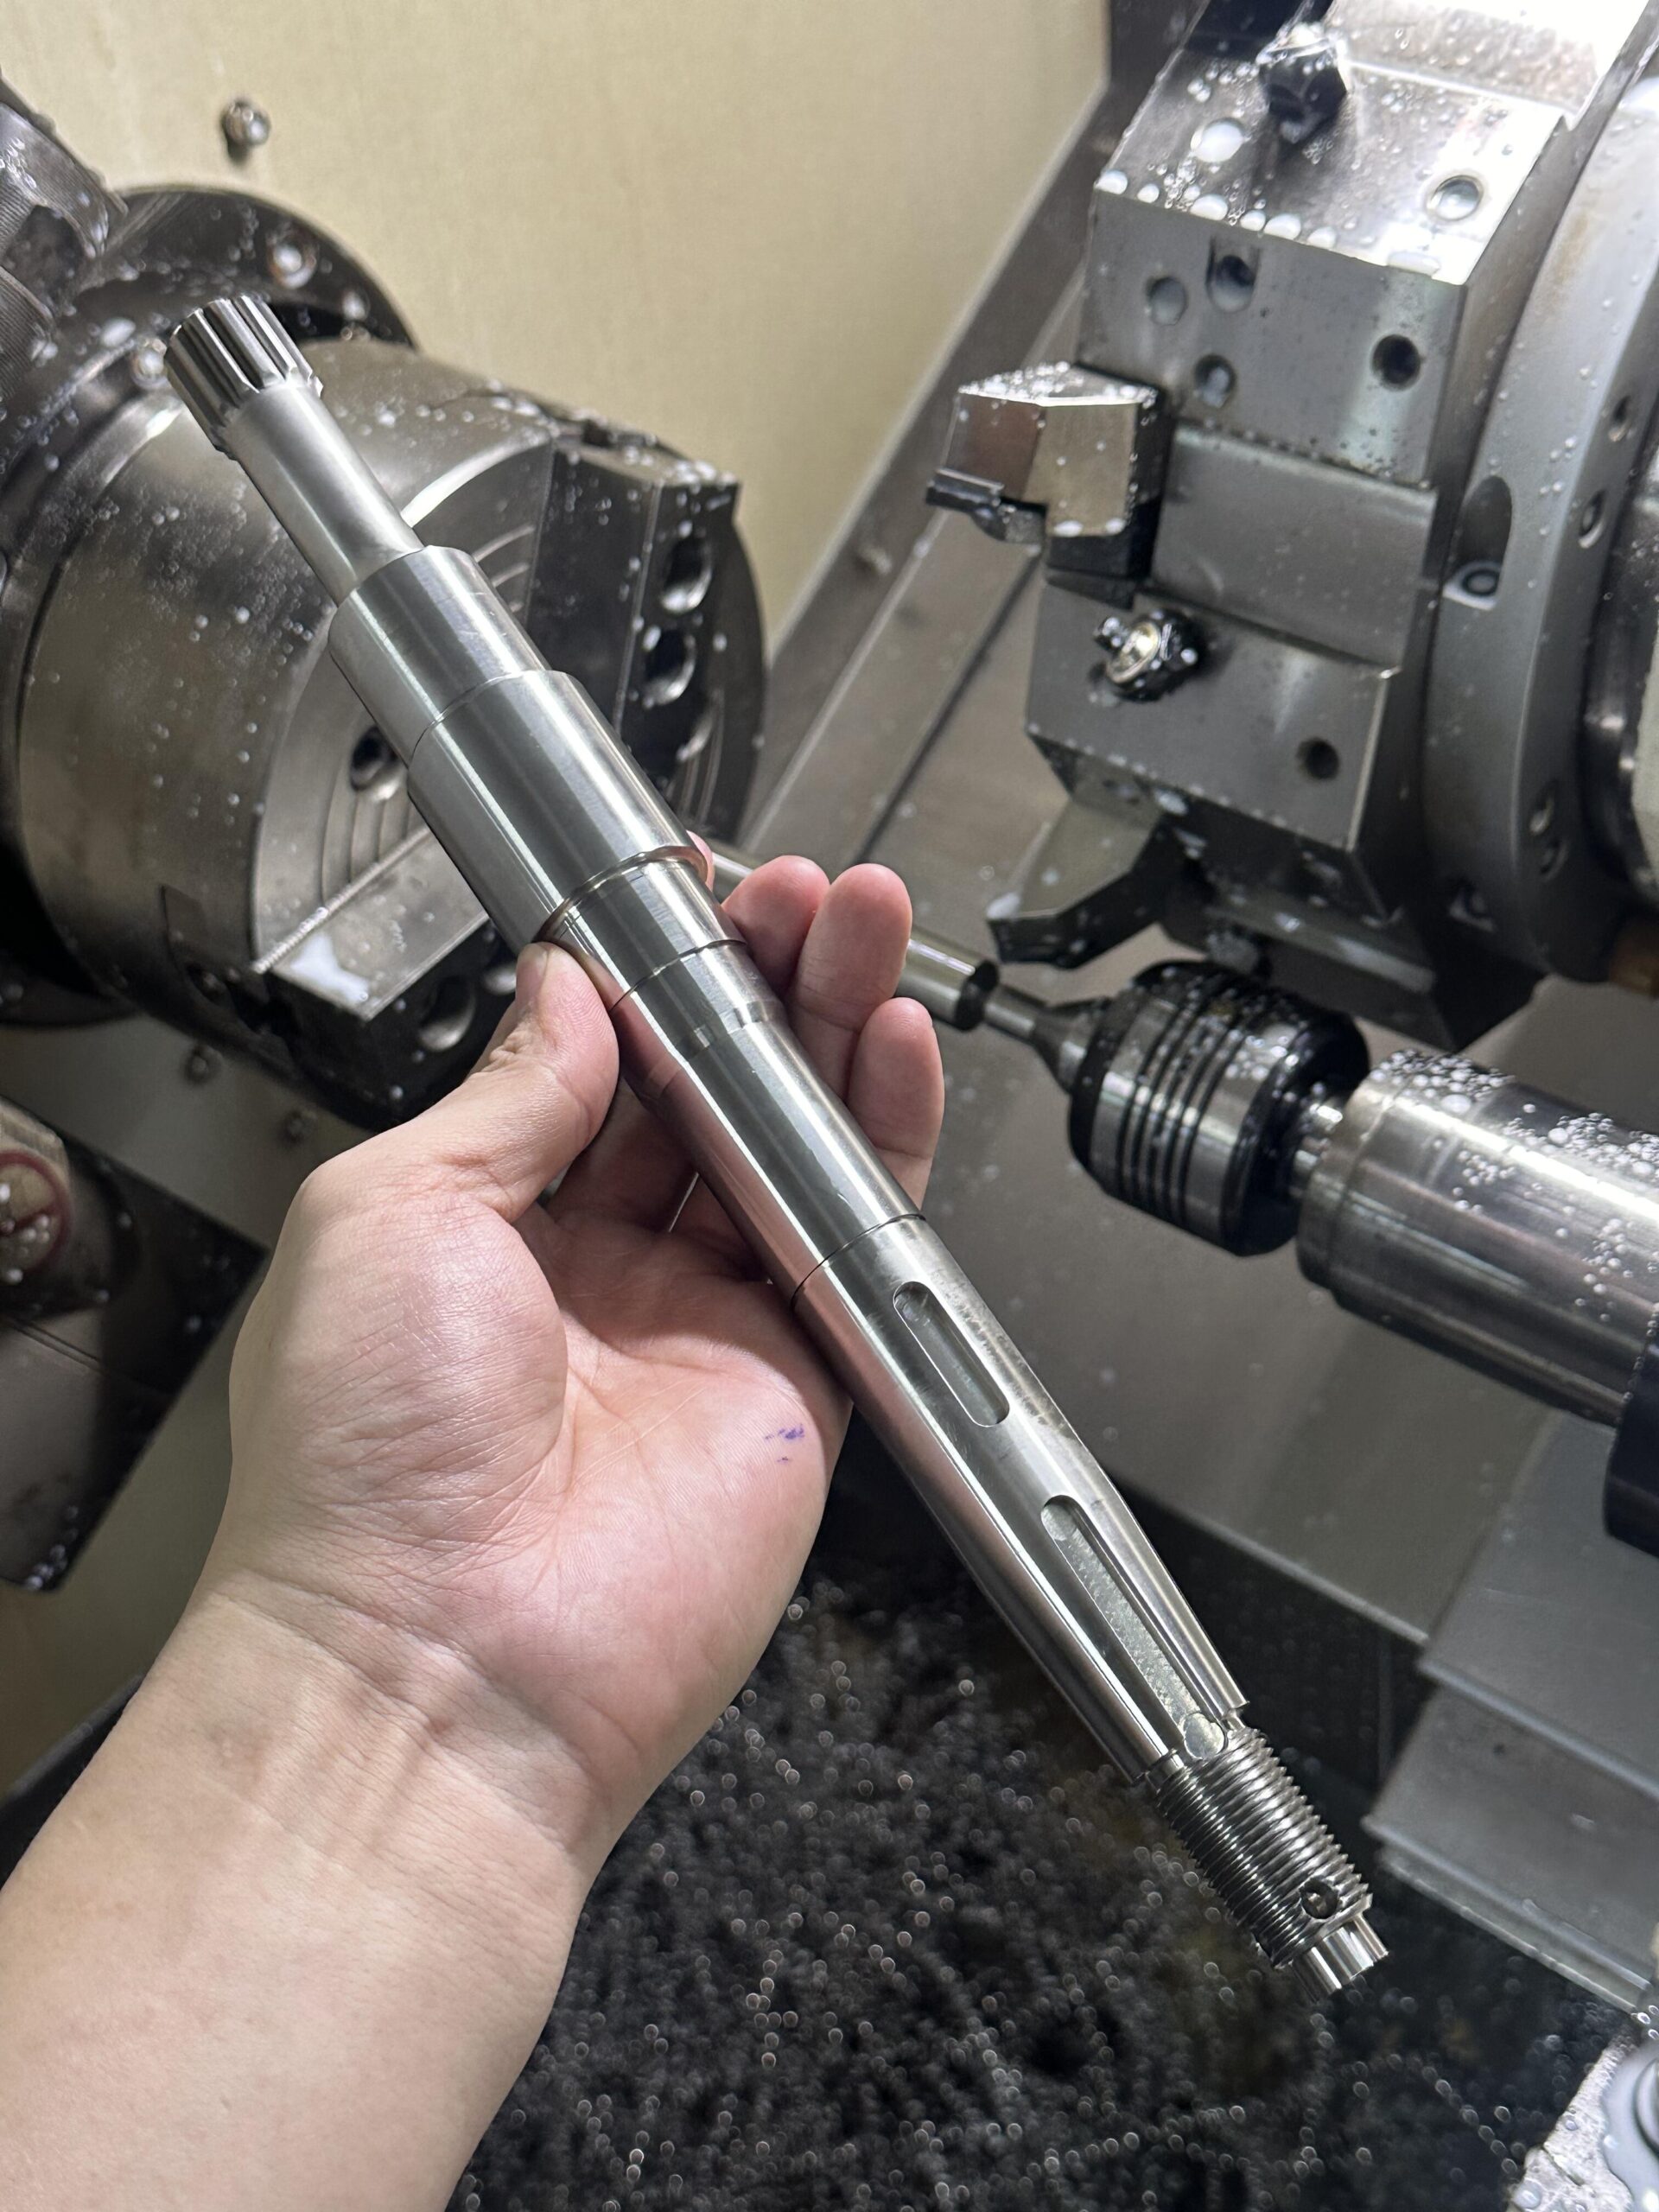
Primary drive and transmission shafts subject to combined torsional, bending, and fatigue loading. Machined from 42CrMo4 (AISI 4140 equivalent) billet, quench and tempered (Q&T) to HRC 28–32 or HRC 32–36 to achieve 950–1080 MPa tensile strength. Bearing seat OD tolerances k6/m6 with TIR ≤0.01 mm between bearing journals, measured and documented. DIN 6885 parallel keyway with width P9/depth JS9 tolerance; angular position ±0.1°. Shoulder fillet radii ≥R1.5 mm at all diameter transitions to maximise fatigue life at stress-concentration zones. Finish-ground bearing seats after Q&T to restore dimensional accuracy lost to heat-treatment distortion. Spigot bore H7 on hollow-bored versions. Material certificate and heat treatment record supplied with every order.
42CrMo Q&T HRC 32k6 · TIR ≤0.01mm950–1080 MPaGround post-HT
42CrMo4 · 40Cr · SAE 4340Get Quote
Input Shaft Gearbox Drive Train 42CrMo CNC
ALS-002
SHAFTS / 002
Input Shafts
Gearbox and drive train input shafts. Spigot pilot bore H7; bearing seat k6; TIR ≤0.01 mm. Q&T 42CrMo. Front end spline or keyway for coupling engagement; rear end integrated pilot or journal for first gear/stage support bearing.
H7 spigot boreQ&T 42CrMo
42CrMo · 40CrGet Quote
Output Shaft Gearbox Drive 42CrMo Close Tolerance CNC
ALS-003
SHAFTS / 003
Output Shafts
Drive output shafts with close-tolerance bearing seats and output coupling interface. Keyway DIN 6885 or spline DIN 5480. Q&T 42CrMo HRC 28–36. Case hardened journal option for high-wear output engagement. Induction hardening of output journal available.
Q&T · IH option
42CrMo · 40CrGet Quote
Spline Shaft DIN 5480 Involute CNC Alloy Steel 20CrMnTi
ALS-004
SHAFTS / 004
Spline Shafts
Involute spline shafts to DIN 5480 or ANSI B92.1, profile tolerance class 7. 20CrMnTi case carburised: case depth 0.8–1.2 mm, surface HRC 58–62, core HRC 30–38. Spline hobbed before carburising; spline profile verified by gear-measuring machine post-HT.
Case HRC 58–62DIN 5480 class 7
20CrMnTi · 42CrMoGet Quote
Gear Shaft Integral Pinion CNC Alloy Steel 20CrMnTi Case Carburised
ALS-005
SHAFTS / 005
Gear Shafts
Integral pinion-shaft with hobbed gear teeth on shaft body. 20CrMnTi case carburised to HRC 58–62; bearing seat h6 ground post-HT. Gear tooth quality DIN 3962 class 8 standard; class 6 by grinding available. Profile verified by gear-measuring machine.
HRC 58–62DIN 3962 class 8
20CrMnTi · 17CrNiMo6Get Quote
Materials: 42CrMo4 · 40Cr · 20CrMnTi · 17CrNiMo6 · SAE 4340
Request All 5 →
Coupling Flanged Sleeve Connecting Rod Fork Steering CNC Alloy Steel
Couplings, Sleeves & Linkages5 Products · ALS-006 to 010Quote →
High-strength couplings, flanged sleeves, connecting rods, fork connectors, and steering connectors — the torque-carrying and motion-linking hardware of high-load drive trains and steering systems. Coupling bore H7; OD runout ≤0.02 mm. Connecting rod bore centreline ±0.02 mm. Fork pin bore H7/H8; perpendicularity ≤0.02 mm. All parts Q&T 42CrMo or 40Cr with material certificate.
42CrMo Connecting Rod CNC Alloy Steel Big End Small End H7 Bore Fatigue
ALS-011
LINKAGES / 011 — FEATURED
Connecting Rods
Alloy steel connecting rods for crank-slider mechanisms, reciprocating compressors, press-forging machines, and engine rebuild applications. Machined from 42CrMo forging or billet, Q&T to HRC 28–35. Big-end and small-end bore centreline tolerance ±0.02 mm — the specification that controls kinematic accuracy of the assembled mechanism. H7 bore on small (pin) end; H7 on big end before bearing bore honing. Fatigue-rated transition radii R ≥ 1.5 mm at bore-to-shank intersections — not arbitrary chamfers. Bolt flange face flatness ±0.01 mm on split big-end versions. Shot-peening available for maximum fatigue life in high-cycle reciprocating applications. CMM bore centreline measurement report included.
CL ±0.02mmH7 pin boreR≥1.5mm filletShot-peen option
42CrMo · SAE 4340 · 40CrGet Quote
High-Strength Coupling 42CrMo H7 Bore OD Runout CNC
ALS-006
LINKAGES / 006
High-Strength Couplings
42CrMo rigid and jaw coupling halves, Q&T HRC 28–35. H7 bore; OD runout ≤0.02 mm for high-speed balance. DIN 6885 keyway. Balancing groove on OD. For torque levels where standard 45# couplings are undersized.
H7 bore42CrMo Q&T
42CrMo · 40CrGet Quote
Flanged Sleeve Hub 42CrMo H7 Bore Flange Face CNC Alloy
ALS-007
LINKAGES / 007
Flanged Sleeves
Heavy-duty flanged hub sleeves and shaft-coupling hubs from 42CrMo. H7 bore; flange face flatness ±0.02 mm; bolt pattern ±0.01 mm. Keyway and set-screw boss options. Q&T or through-hardened options.
±0.02mm flange
42CrMo · 40Cr · SS440CGet Quote
Fork Yoke Connector Alloy Steel H7 Pin Bore Perpendicularity CNC
ALS-012
LINKAGES / 012
Fork / Yoke Connectors
Heavy-duty alloy steel clevis yokes and fork-end connectors. Pin bore H7/H8; fork width ±0.05 mm; pin hole perpendicularity ≤0.02 mm to thread shank. Q&T 40Cr HRC 30–38. For high-load linkage joints.
H7/H8 pin boreHRC 30–38
40Cr · 42CrMoGet Quote
Steering Connector Universal Joint Yoke Alloy Steel Spline CNC
ALS-013
LINKAGES / 013
Steering Connectors
Steering joint and universal-joint yoke bodies. Spline, D-bore, or keyway interface. 40Cr Q&T HRC 28–35. Surface treatment: zinc phosphate + oil standard; hard chrome on journal pin for wear resistance. Custom to OEM drawing.
Spline / D-boreOEM drawing
40Cr · 42CrMoGet Quote
Materials: 42CrMo · 40Cr · SAE 4340 · SS440C
Request All 5 →
Gear Blank Sprocket Cam Eccentric Carburised Gear CNC Alloy Steel
Gears, Sprockets & Cams5 Products · ALS-014 to 018Quote →
Gear blanks, sprockets, cams, eccentric wheels, and carburised gears — the profile and motion-generation hardware of power transmission systems. Gear blank OD h6 with bore-to-OD runout ≤0.01 mm; face parallelism ±0.01 mm for hobbing accuracy. Carburised gear: 20CrMnTi, case depth 0.8–1.2 mm, HRC 58–62. Sprocket teeth cut to ISO 606 or ANSI B29.1. Cam profiles CNC-contoured to ±0.02 mm.
Carburised Gear 20CrMnTi CNC Case Depth HRC 58-62 Hobbed DIN 3962
ALS-019
GEARS / 019 — FEATURED
Carburised Gears
Case carburised and hardened gears in 20CrMnTi (standard) or 17CrNiMo6 (high-load automotive). Gas carburising to case depth 0.8–1.2 mm; quench and temper to surface hardness HRC 58–62 and core hardness HRC 30–38. Gear teeth hobbed on precision turning centre before carburising — blank bore H7, OD runout ≤0.01 mm. After carburising and quench, bore and reference faces ground to remove heat-treatment distortion: bore H7 maintained; face runout ≤0.01 mm. Tooth profile quality DIN 3962 class 8 (hobbed); class 6 after gear grinding. Profile and lead error verified by gear-measuring machine. CMM dimensional report for bore and face features. Material certificate with chemical composition per heat number. Applications: gearbox reduction stages, differential spur gears, planetary carriers, and timing gears.
HRC 58–62 surfaceCase 0.8–1.2mmDIN 3962 class 8Gear-machine verified
20CrMnTi · 17CrNiMo6 · 20CrGet Quote
Sprocket Chain CNC Alloy Steel ISO 606 Bore H7 Keyway
ALS-015
GEARS / 015
Sprockets
Custom chain sprockets to ISO 606 (metric) or ANSI B29.1 (inch). Bore H7; keyway DIN 6885. 45# normalised or 40Cr Q&T HRC 40–45 for wear-resistant tooth flanks. Pitch verified by pin-measurement method.
ISO 606 / ANSI B29.1Pin-measured
45# · 40Cr · GCr15Get Quote
Cam Profile CNC Alloy Steel Case Hardened Working Surface
ALS-016
GEARS / 016
Cams
CNC contour-milled cams. Lift curve profile tolerance ±0.02 mm; bore H7; working surface case hardened HRC 55–60 for wear resistance. Base circle and rise/fall profile verified by CMM. Custom cam curves to drawing or point-cloud data.
Profile ±0.02mmHRC 55–60
40Cr · GCr15 · 42CrMoGet Quote
Eccentric Wheel Disc CNC Alloy Steel Eccentricity Tolerance Hardened
ALS-017
GEARS / 017
Eccentric Wheels
Eccentric discs and offset cams. Eccentricity tolerance ±0.01 mm; bore H7; OD working surface hardened and ground Ra ≤0.4 μm. Used in reciprocating mechanism drive stages, adjustable stroke mechanisms, and off-axis drive applications.
Eccentricity ±0.01mmGround OD
40Cr · GCr15Get Quote
Materials: 20CrMnTi · 17CrNiMo6 · 40Cr · GCr15 · 45#
Request All 5 →
Manufacturing Capability

Why Alloy Steel Transmission Parts Demand
a Specialist Machining Partner

🔥
Case Carburising — 20CrMnTi to HRC 58–62
Gas carburising to case depth 0.8–1.2 mm followed by quench to HRC 58–62 surface, HRC 30–38 core. We manage the complete carburising cycle — part machining → carburising → quench → post-HT precision grinding of bore and faces. Case depth and hardness test report included.
Case 0.8–1.2mmHRC 58–62Post-HT grind
⚙
Bearing Seat Ground Post-Q&T — TIR ≤0.01mm
Bearing seats ground after Q&T heat treatment to restore dimensional accuracy lost to heat-treatment distortion. TIR ≤0.01 mm measured and documented — not assumed from machining parameters. The specification that determines bearing life and shaft alignment.
Ground post-HTTIR ≤0.01mmDocumented
🔩
Spline DIN 5480 Class 7 — Gear-Machine Verified
Involute spline profiles to DIN 5480 class 7 verified by gear-measuring machine — not assumed from CNC program. For case carburised spline shafts: hobbed before HT, profile re-verified after HT and grinding. Profile error and lead variation reported.
DIN 5480 class 7Gear-machine checkPost-HT verified
🤖
Robot Joint Coaxiality ≤0.005mm — 5-Axis
Robot arm load joint bore coaxiality ≤0.005 mm in 5-axis single setup. Re-fixturing compounds error to ±0.01–0.05 mm and cannot achieve this specification. Full GD&T CMM report on every robot joint order — bore coaxiality, roundness, flange runout, perpendicularity.
≤0.005mm coaxial5-axis single opGD&T CMM
⚖
42CrMo 1080 MPa — 44% Stronger than 45#
42CrMo Q&T to HRC 32 achieves 1080 MPa — 44% higher than 45# carbon steel (750 MPa). For fatigue-loaded transmission shafts and connecting rods, the difference in fatigue limit (endurance limit) is even larger — typically 60–80% improvement. Not cosmetic — sized correctly, alloy steel enables smaller and lighter parts for the same load.
1080 MPa Rm44% vs 45#Superior fatigue
📋
PPAP & SPC — Automotive Production
PPAP documentation (Part Submission Warrant, Control Plan, FMEA, measurement system analysis) available for automotive OEM orders. SPC and Cpk reporting for critical dimensions in series production. OEM-grade documentation for powertrain and chassis components.
PPAP availableSPC CpkOEM-grade docs
Precision Specifications

Tolerances & Heat Treatment Reference — Alloy Steel Parts

📐
Tolerances by Feature
Bearing Seat OD
k6 / m6
Shaft TIR
≤0.01 mm
Bore (Housing)
H7
Robot Joint Coax.
≤0.005 mm
Gear Blank Runout
≤0.01 mm
Cam Profile
±0.02 mm
Eccentricity
±0.01 mm
General Dim.
±0.05 mm
🔥
Grade & Heat Treatment Reference
42CrMo Q&T
1080 MPa
HRC 32 condition. High-strength shafts, couplings, robot joints. Best all-round alloy transmission grade.
40Cr Q&T
900 MPa
HRC 28 condition. Lighter-duty shafts, forks, connectors. Good machinability, economical.
20CrMnTi Carb.
HRC 58–62
Case depth 0.8–1.2mm. Standard carburising grade for gear teeth, spline shafts. Core HRC 30–38.
GCr15 Hardened
HRC 60–64
Through hardened bearing steel for wear-resistant bushings, cam followers, roller shafts.
17CrNiMo6
HRC 58–62
Premium case carburising steel for high-load automotive gears. Better core toughness than 20CrMnTi.
SAE 4340
HRC 38–42
Ultra-high strength, 1200 MPa+. Connecting rods and robot joints in extreme load applications.
Material Selection

Alloy Steel Grades for Power Transmission Parts

Alloy steel grade selection for transmission parts is dominated by hardenability, fatigue limit, and case carburising behaviour.

MAT / 01
42CrMo4 (AISI 4140)
1080 MPa · HRC 32 Q&T · Best all-round
Standard grade for high-strength transmission shafts, couplings, and load joints. 42% chromium + 0.2% molybdenum improve hardenability through larger cross-sections than 40Cr. Best combination of strength, toughness, and machinability.
ShaftsRobot Joints
MAT / 02
40Cr
900 MPa · HRC 28 Q&T · Economical
Lighter-duty shafts, forks, and connectors where 42CrMo is over-specified. Good hardenability for sections up to 50 mm diameter. Economical choice for medium-load power transmission parts.
ForksSprockets
MAT / 03
20CrMnTi
Case HRC 58–62 · Core HRC 30–38 · Standard carburising grade
Chinese-standard carburising grade for gear teeth, spline shafts, and transmission parts requiring hard case + tough core. Gas carburising to case depth 0.8–1.2 mm. Standard for automotive gearbox gears. Equivalent to 20MnCr5 (European).
GearsSpline Shaft
MAT / 04
17CrNiMo6 (16MnCr5)
Case HRC 58–62 · Superior core toughness
Premium European carburising steel for high-load automotive gears. Nickel addition improves core impact toughness vs 20CrMnTi — preferred for differential and transmission gears under shock loads. PPAP documentation available for automotive OEM orders.
Auto GearsPPAP
MAT / 05
GCr15 (SUJ2 / 52100)
HRC 60–64 · Highest wear resistance · Bearing steel
Bearing steel for the highest wear resistance applications — wear bushings, cam followers, roller shafts. Through hardened to HRC 60–64. Better wear life than 40Cr for parts in rolling and sliding contact.
Wear BushingsCams
MAT / 06
SAE 4340 (EN24)
1200+ MPa · Ultra-high strength · Deep hardening
Ultra-high strength alloy for connecting rods and robot joints in extreme load applications. Chromium-nickel-molybdenum ensures through-hardening in sections up to 150 mm diameter. Best fatigue resistance of all common alloy steels. Used where 42CrMo cannot reach the required strength after Q&T.
Con RodsRobot Joints
Surface Treatments

Corrosion & Wear Protection for Alloy Steel Transmission Parts

Surface treatment selection for alloy steel transmission parts must preserve dimensional tolerance — particularly for bearing seats and gear flanks.

🛡
Manganese Zinc Phosphate + Oil
The standard surface treatment for alloy steel transmission parts. Excellent corrosion protection, friction reduction, and oil retention in gear and sliding contact applications. Zero dimensional change — preserves all ground tolerances. Standard for shafts, gears, and couplings.
ShaftsGears
🔲
Black Oxide
Hot black oxide for minimal corrosion protection with absolute zero dimensional change (<1μm). Used for precision ground bearing seats and cam profiles where any coating thickness would degrade tolerance. Applied after grinding.
Bearing SeatsCam profile
✦
Hard Chrome Plating
Hard chrome 10–30 μm, HV 900–1200, Ra ≤0.1 μm after grinding. For shaft journals, connecting rod bores, and cam working surfaces requiring maximum wear resistance. Chromium-free (PVD TiN, CrN) alternatives available for RoHS applications.
Shaft journalsCam OD
💧
Electroless Nickel (EN)
Uniform EN 25–75 μm for hydraulic connectors and gearbox parts in corrosive or hydraulic fluid environments. Corrosion resistance + surface hardness ~500 HV. Requires tolerance allowance — confirmed at DFM stage before machining.
Hydraulic partsCorrosive env.
🔥
Gas / Plasma Nitriding
Gas or plasma nitriding of 42CrMo shafts to surface hardness HV 900+ with case depth 0.1–0.3 mm. Minimal distortion vs carburising — suitable for shafts that cannot be ground after heat treatment. Improves fatigue limit and wear resistance without sacrificing dimensional accuracy.
42CrMo ShaftsNo grinding needed
🎨
Zinc Phosphate + Primer
Zinc phosphate base coat + epoxy primer for heavy structural connectors, hydraulic equipment connectors, and alloy steel parts in outdoor environments. Top-coat paint in any RAL colour optional. Standard for outdoor transmission housings and frames.
StructuralOutdoor
Our Advantage

Why Drive Train Engineers Specify Our Alloy Steel Parts

HT
Heat Treatment + Post-HT Grinding — One Supplier
Alloy steel transmission shafts require bearing seats ground after Q&T to remove heat-treatment distortion. We manage Q&T, carburising, and post-HT precision grinding as one complete order. You receive a finished, ground, certified part — not a heat-treated blank requiring separate grinding sourcing.
1080
42CrMo 1080 MPa — Properly Documented
42CrMo Q&T to HRC 32 achieves 1080 MPa tensile strength — 44% higher than 45# carbon steel. Material certificate with chemical composition and mechanical properties per heat number. Heat treatment record with process parameters and hardness test results. Not claimed without evidence.
5-Ax
Robot Joint ≤0.005mm Coaxiality — 5-Axis
Alloy steel robot arm load joints machined in 5-axis single setup for bore coaxiality ≤0.005 mm. Full GD&T CMM report on every order — not just dimensional pass/fail. The joint that carries cyclic combined loading needs documented geometry, not assumed accuracy.
PPAP
Automotive-Grade Documentation Available
PPAP documentation, SPC Cpk reporting, and OEM material grade sourcing (17CrNiMo6, SAE 4340, 16MnCr5) available for automotive OEM production programmes. The documentation rigor that OEM supply chains require — and that most job shops cannot provide.
Frequently Asked Questions

Alloy Steel Transmission Parts — Common Questions

Technical questions about steel grades, heat treatment, gear standards, and supply chain for alloy steel power transmission parts.

We machine all standard alloy steel grades: 42CrMo4 (AISI 4140 equivalent) — standard for high-strength transmission shafts, 950–1080 MPa, Q&T. 40Cr — lighter-duty shafts and connectors, 900 MPa. 20CrMnTi — standard Chinese carburising grade for gear teeth and spline shafts, case HRC 58–62. 17CrNiMo6/16MnCr5 — premium automotive carburising grades, better core toughness. GCr15 (bearing steel) — wear bushings and cam followers, HRC 60–64. SAE 4340 — ultra-high strength connecting rods and robot joints, 1200+ MPa.
We manage all heat treatment end-to-end: quench & temper (Q&T) of 42CrMo/40Cr to HRC 28–42; gas carburising of 20CrMnTi to case depth 0.8–1.2 mm, surface HRC 58–62; induction hardening of bearing seats and gear flanks for selective hardening; through hardening of GCr15 to HRC 60–64; gas/plasma nitriding of 42CrMo to HV 900+; and annealing for stress relief. Heat treatment record (process cert + hardness test) included with every heat-treated order.
Involute splines hobbed to DIN 5480 (metric) or ANSI B92.1 (inch), profile tolerance class 7 as standard; class 5–6 by post-HT grinding. For case carburised spline shafts: hobbed before carburising, then profile re-verified by gear-measuring machine after HT and grinding. Straight-sided splines to DIN 5461 by broaching or milling. All spline profiles verified by gear-measuring machine — not assumed from CNC program.
Gear blank: OD h6 (hobbing reference); bore H7; face-to-face parallelism ±0.01 mm; bore-to-OD runout ≤0.01 mm. Gear shaft: bearing seat OD k6/m6; TIR ≤0.01 mm between journals. For carburised gear shafts: bearing seats finish-ground after HT to restore tolerance. CMM dimensional report with every gear blank and gear shaft order.
Yes. Connecting rods: 42CrMo Q&T; bore centreline ±0.02 mm; H7 pin bore; fatigue-rated fillet radii ≥R1.5 mm; shot-peening option. CMM bore centreline report included. Cam profiles: CNC contoured to ±0.02 mm; working surface case hardened HRC 55–60; profile verified by CMM. Eccentric wheel eccentricity tolerance ±0.01 mm; ground working surface.
Standard carbon steels (45#, Q235) achieve 600–750 MPa tensile strength. Alloy steels (42CrMo, 40Cr, 20CrMnTi) achieve 900–1200 MPa after heat treatment — 50–100% higher. The key difference is hardenability — alloy steel can be through-hardened in larger cross-sections than carbon steel. For fatigue-loaded transmission shafts, couplings, and gear teeth, alloy steel is specified because carbon steel cannot achieve the required fatigue life at the applied load without disproportionate size and weight increase.
Yes. We supply gear blanks machined ready for hobbing, or complete gears with teeth hobbed, shaved, or ground in-house or through certified gear-cutting partners. Gear quality: DIN 3962 class 8 standard (commercial hobbed); class 6 after shaving or grinding. Sprockets to ISO 606 (metric) and ANSI B29.1 (inch) with bore H7 and keyway. All gear geometry verified by gear-measuring machine.
MOQ is 1 piece. Standard parts without heat treatment: 5–10 working days. Parts requiring Q&T: add 5–7 working days. Parts requiring case carburising: add 7–10 working days. Complex multi-feature parts (gear shafts, robot joints): 10–15 working days plus HT time. Automotive production batches: lead times agreed in advance — please discuss your forecast. All parts shipped with material certificate and heat treatment record.

Structured data (FAQPage + ItemList + Product schema) embedded in page head · Eligible for Google FAQ rich results

Get a Quote

Send Your Drawing.
Get a Quote.

Every enquiry includes a DFM review — tolerance feasibility, material confirmation, and process approach confirmed before production starts. MOQ 1 piece.

24hr
Quote Response
MOQ 1
Prototypes OK
ISO
9001:2015
📐
DFM Review on Every Enquiry
Tolerance feasibility, fixturing strategy, and material confirmation. Specific, actionable feedback — not generic pushback.
🎯
First Article Inspection — Standard
FAI report on every new run. Material certs and surface treatment certs included with every shipment.
🔄
Same Process: Prototype to Production
Process plan from your prototype applies to production batches. No re-qualification when you scale.
⚙
3 / 4 / 5-Axis CNC + Turning
Complex structural parts, shafts, housings, and transmission components. Metals and engineering plastics.
ISO 9001:2015 3/4/5-Axis Milling CNC Turning CMM Inspection Global Delivery